For importers, an AQL inspection in China is a structured way to decide whether a production lot is ready to ship—not a substitute for choosing and managing a capable supplier. The process uses a defined sample, agreed defect categories, and acceptance limits so buyer and factory can evaluate results against the same purchase specification. Used well, it catches visible workmanship issues, quantity gaps, packaging mistakes, and selected functional failures before goods leave the country. It also creates evidence for a corrective-action discussion. The buyer still needs to set requirements, verify the supplier, select suitable tests, and connect inspection findings to compliance, delivery, and landed-cost decisions.
What AQL means in a China sourcing order
AQL, or Acceptance Quality Limit, is a sampling concept used to establish how many defects may be found in a sample before a lot is accepted or rejected. It does not mean that a shipment is guaranteed to contain no defects, nor does it describe the percentage of defective units that will certainly be delivered. The sampling plan must be agreed with the product specification, lot size, inspection level, and defect definitions. ISO 2859-1 is a widely used reference for attribute-based sampling procedures [1]. Treat AQL as a decision rule, not as a quality target by itself.
In China sourcing, the practical starting point is a written inspection standard attached to the purchase order. Describe materials, dimensions, colors, labels, accessories, workmanship, carton marks, and critical functions in measurable terms. Then classify defects as critical, major, or minor and assign acceptance numbers separately where appropriate. A factory and buyer may otherwise use the word ‘AQL’ while judging different conditions. Clear photographs, approved samples, drawings, and packaging instructions reduce ambiguity and make the report useful if rework, sorting, replacement, or a shipment hold becomes necessary.
How the sampling process works
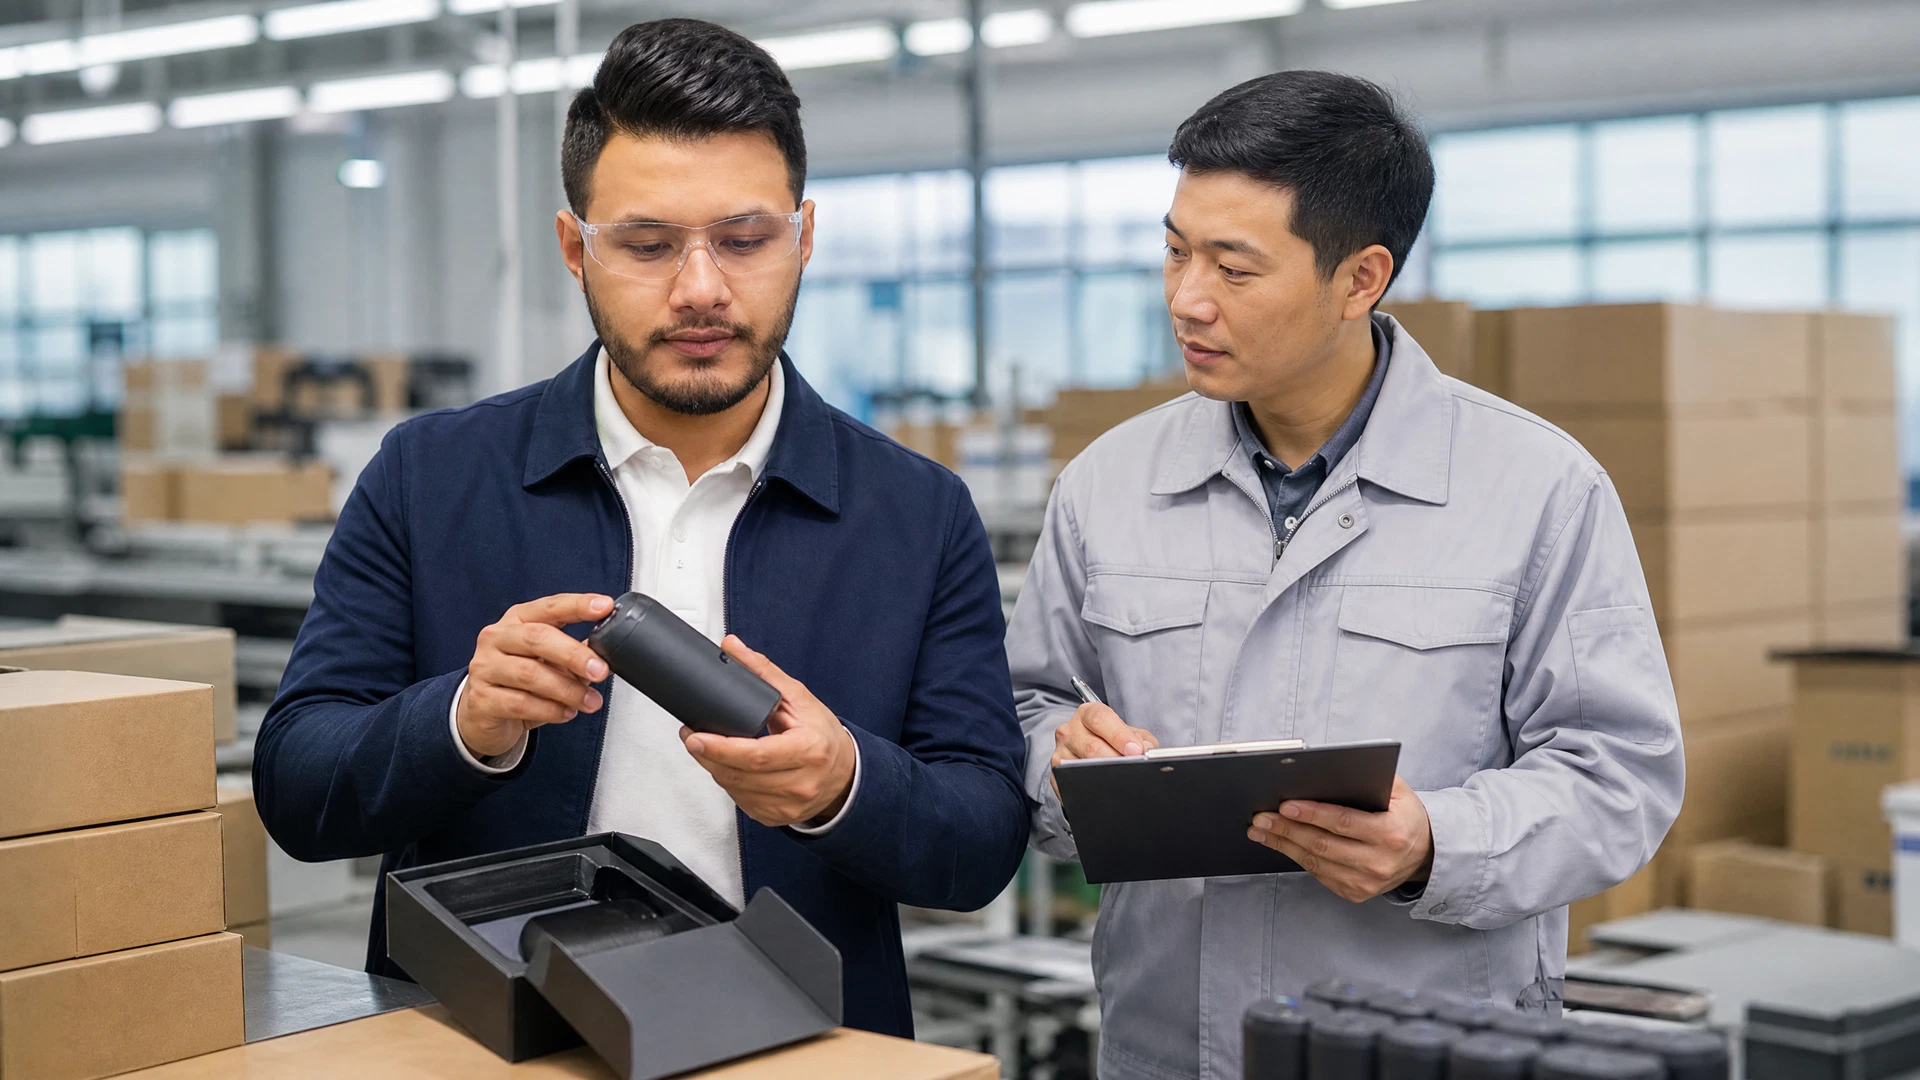
An inspector normally confirms the finished quantity, identifies the production lot, and selects units using a documented sampling plan rather than choosing only convenient cartons. The lot size and selected inspection level determine a code letter and sample size under the applicable standard or buyer procedure. Sampled units are then checked against the agreed checklist, with results recorded by defect type. For a defensible result, the report should show the lot quantity, sample quantity, locations visited, inspection date, equipment used, measurements, photographs, and the acceptance decision.
Sampling is efficient because it gives a buyer information without opening and testing every unit, but it introduces a chance of overlooking problems. That risk is why the plan should match the product’s consequences of failure. A simple visual check may suit low-risk accessories, while electrical goods, children’s products, food-contact items, or load-bearing hardware may need laboratory testing, safety verification, or a larger functional program. An inspector should never be asked to infer requirements from a vague product name or an old quotation.
Choosing defect limits that protect buyers
Defect limits should reflect how a customer experiences the product and how a failure affects safety, use, returns, or reputation. Critical defects generally require zero acceptance and an immediate escalation path, but the exact definition belongs in the specification and applicable regulatory framework. Major defects can make an item unusable, visibly unacceptable, or materially different from the order; minor defects may affect appearance without preventing normal use. Avoid copying generic values without review. A buyer should explain why a limit is appropriate for the market, product category, and sales channel.
The inspection plan also needs rules for repeated defects and defect counting. State whether two problems on one unit count as two defects, whether a missing component causes a functional failure, and how mixed colors or sizes are sampled. Include tolerances for dimensions and weight, plus a method for measuring them. For appearance, define acceptable variation using a sealed sample or approved golden sample. These details help separate a negotiable cosmetic issue from a shipment that needs controlled rework and a new inspection.
What a pre-shipment inspection should cover
A pre-shipment inspection is most informative when production is substantially complete and packing has begun, because the buyer can assess finished goods, labeling, and carton configuration together. The inspector may verify quantity, workmanship, dimensions, construction, color, assortment, accessories, operation, packaging, and shipping marks. The exact scope depends on the order. For products with measurable performance, specify the test method, sample quantity, test duration, acceptance criterion, and whether a destructive test is permitted. Never treat a visual pass as proof of chemical, microbiological, or electrical compliance.
The inspector should compare findings with the purchase order and approved reference materials, not with personal expectations. Photographs should identify the observed condition without exposing confidential information unnecessarily. A report that says ‘poor quality’ is weak; a report that identifies carton 12, a seam location, measured tolerance, defect classification, and sample result supports action. If the inspection occurs before full packing, record what remained unfinished and require a follow-up check for quantity, labels, or packaging changes before release.
Using inspection results with supplier verification
An AQL result is one data point in supplier verification. Before placing repeat orders, review the factory’s legal identity, manufacturing address, production capability, subcontracting practices, quality system, traceability, and responsiveness to corrective actions. Confirm that the inspected facility is the one producing the goods, especially when a trading company coordinates the transaction. Ask for controlled versions of specifications and test reports, and check whether certificates identify the correct model, material, factory, and date. A polished inspection report cannot compensate for an unclear supply chain or unsupported compliance claim.
When defects exceed the agreed acceptance number, pause the shipping decision and request a root-cause response with containment, correction, and preventive action. Depending on the issue, the remedy may involve sorting, rework, replacement, a price adjustment, or cancellation under the contract. After corrective work, define exactly what will be rechecked and who pays for it. Keep versions of the report, photographs, approvals, and correspondence in one order file. That documentation improves continuity when staff, suppliers, or logistics providers change.
Connecting AQL findings to compliance and landed cost
Inspection planning should distinguish commercial conformity from regulatory compliance. A dimensional or workmanship check may confirm that goods match the order, while market-entry obligations can require technical files, declarations, labeling, restricted-substance evidence, or accredited laboratory results. The importer remains responsible for understanding the destination market’s rules and allocating responsibilities in the contract. For example, EU product compliance may involve harmonised standards and conformity assessment obligations that are separate from factory inspection [2]. AQL sampling should therefore include document and label checks where those items are part of release criteria.
Finally, translate findings into the shipment economics rather than viewing inspection as an isolated fee. A failed lot can create reinspection charges, labor for sorting, storage, missed vessel cutoffs, expedited freight, customer penalties, and inventory shortages. Build time for corrective action into the purchase schedule and confirm the final packing list, commercial invoice, carton count, and shipping marks after approval. A clear release workflow—inspection pass, document review, payment authorization, and booking confirmation—helps protect cash flow without promising that sampling eliminates every downstream risk.
AQL inspection decisions for common buyer situations
| Buyer situation | Useful inspection emphasis | Release decision to document |
|---|---|---|
| First order with an unfamiliar supplier | Verify facility identity, quantity, workmanship, packaging, and basic function against approved samples | Hold payment or booking until findings and supplier responses are reviewed |
| Repeat order with stable history | Compare defect trends, critical dimensions, assortment, labels, and any prior corrective actions | Release only after the current lot meets the agreed plan and documents are complete |
| Safety-sensitive or regulated product | Use inspection for conformity checks, while arranging specified laboratory or technical tests | Require separate compliance evidence; do not treat an AQL pass as certification |
| Late production before vessel cutoff | Prioritize finished quantity, carton marks, packing list accuracy, and high-risk defects | Record exceptions, owner, deadline, and whether reinspection is required |
| Lot with failed inspection | Quarantine affected goods and identify root cause, sorting scope, and rework status | Approve shipment only after defined corrective checks show conformity |
Buyer checklist
Use this before you request a quote
- Attach an approved sample, drawing, bill of materials, tolerance sheet, packaging guide, and destination-market labeling requirements to the purchase order.
- Agree in writing on lot definition, inspection timing, sampling level, critical/major/minor classifications, AQL values, test methods, and defect-counting rules.
- Verify the actual producing facility, production quantity, subcontracting status, and readiness before scheduling the inspector.
- Review the report against every release criterion, including photographs, measurements, carton marks, packing-list data, and required compliance documents.
- For any failure, quarantine the lot, obtain a written corrective-action plan, and specify the exact rework scope and reinspection requirements before booking shipment.
References
- 1. ISO 2859-1:1999, Sampling procedures for inspection by attributes
- 2. European Commission, CE marking and conformity assessment
- 3. U.S. Consumer Product Safety Commission, Regulatory Robot
This article provides general commercial information, not legal, tax, customs, product-safety, or regulatory advice. Confirm requirements for your product and destination before purchasing or importing.