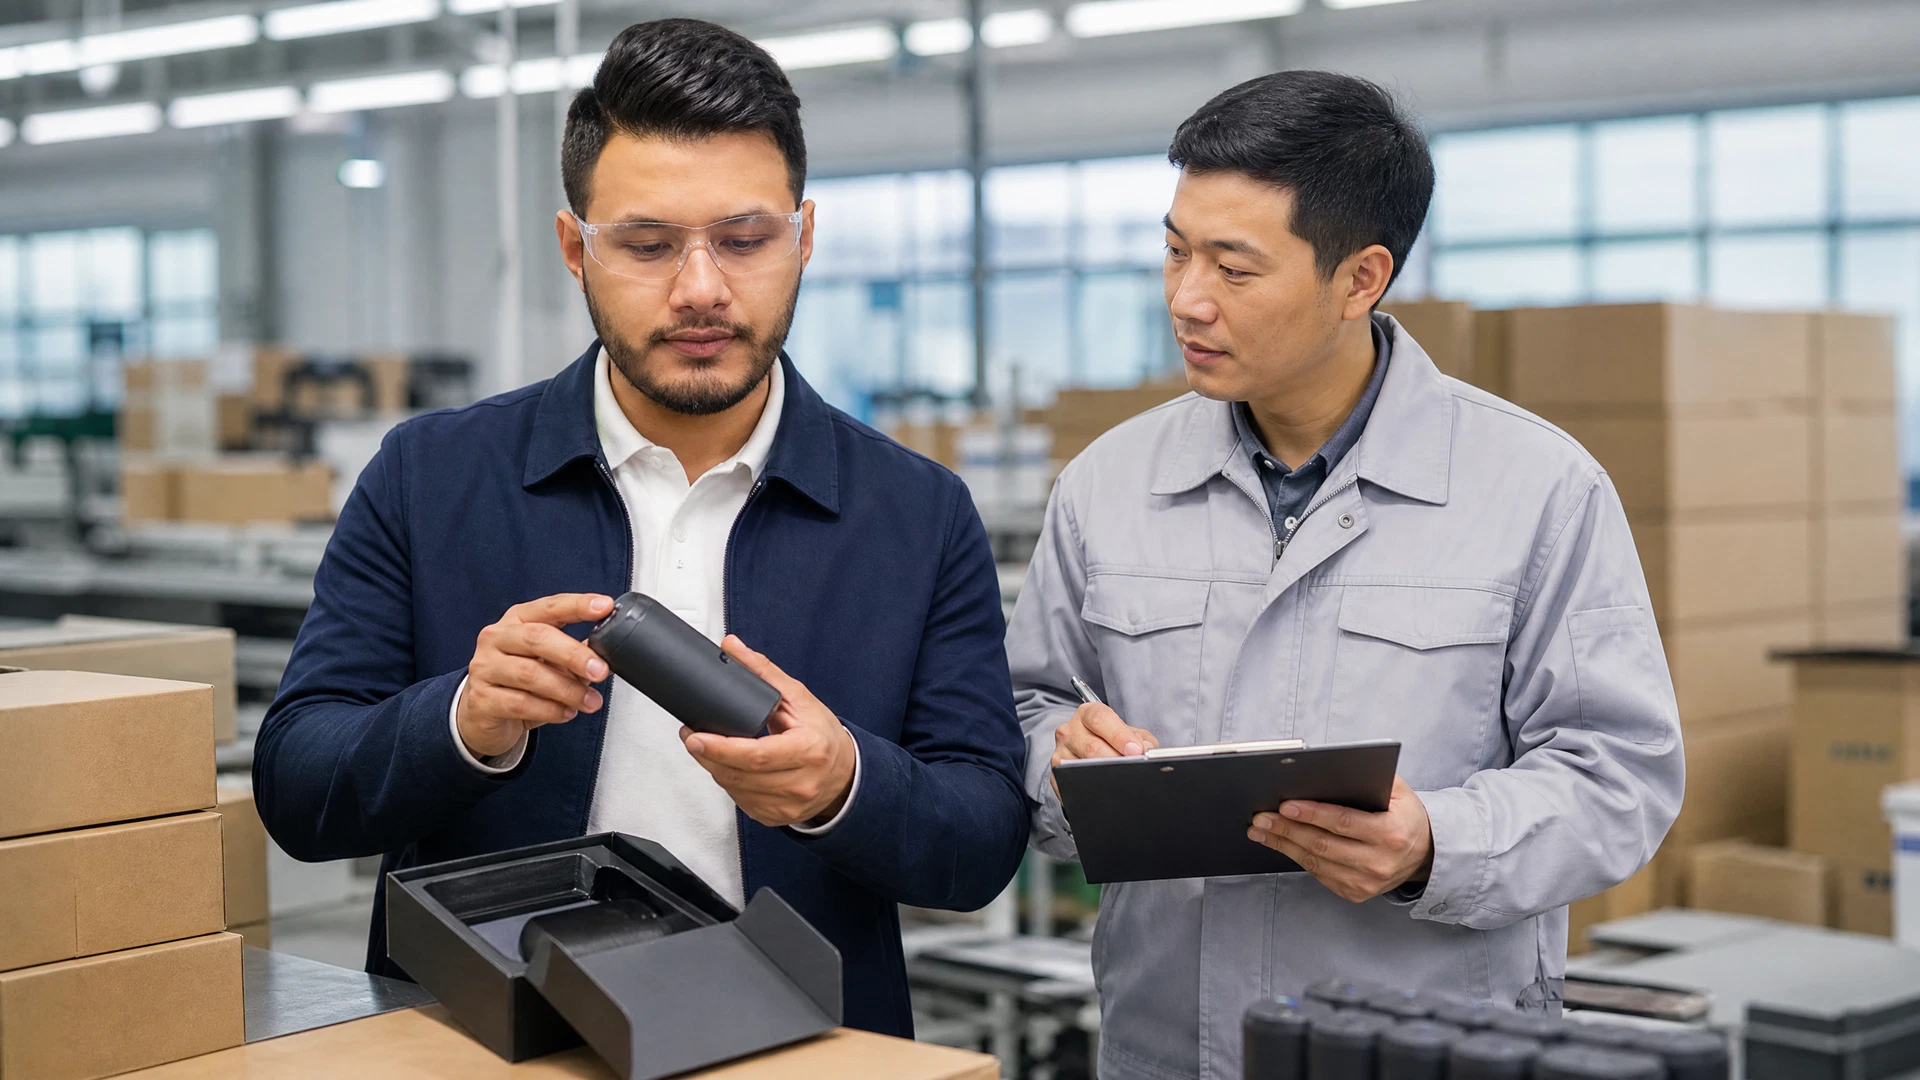
Buying from China does not make inspection a substitute for a clear specification, capable supplier, or realistic logistics plan. Quality control services in China can add an independent checkpoint between production and shipment, but the useful question is not simply whether an inspector can visit a factory. It is whether the inspection plan measures the risks that matter for your product, market, and contract. Start by translating drawings, approved samples, packaging rules, labeling needs, and acceptance limits into a written protocol. Then choose a service provider whose staff, reporting, sampling method, and escalation process fit the order. Treat findings as decision inputs, not as a guarantee of future production.
What a quality control service should cover
A useful provider can support several checkpoints rather than offering only a final visual visit. Supplier audits examine organization, equipment, process controls, records, and capacity; during-production inspections look for early defects while correction is still possible; pre-shipment inspections sample finished goods; and container loading checks confirm quantity, assortment, packaging, and seal details. These services answer different questions. An audit asks whether the factory appears able to produce consistently, while a product inspection asks whether a defined batch meets your agreed requirements. Combining them should reflect risk, order value, lead time, and product complexity.
Ask for a sample anonymized report before appointing anyone. It should show the purchase order, factory identity, production status, sample size, defect classification, photographs, measurements, test results, nonconformities, and a clear disposition such as pass, fail, or pending evidence. A polished dashboard is less important than traceability: the report must let your team connect each observation to a specification and decide what happens next. Confirm whether the provider uses its own personnel, how conflicts of interest are managed, and whether a reinspection follows the same protocol rather than quietly changing the standard.
Turn specifications into an inspection protocol
Inspection becomes reliable only when “good quality” is converted into observable criteria. Provide a controlled specification with revision number, drawings, materials, dimensions, colors, functions, workmanship examples, packaging configuration, carton marks, and required records. Identify critical, major, and minor defects in plain language, but do not copy generic defect limits without considering the product. For a molded component, flash and warpage may matter; for a textile, shade variation and seam strength may matter. Attach approved samples or boundary samples, and state which document prevails if a sample conflicts with a later drawing.
Define what the inspector may measure, test, open, operate, or photograph. Include calibrated instruments where dimensions matter, test conditions for performance checks, and a plan for samples that are unavailable or not yet packed. If laboratory testing is necessary, specify the method, sample custody, laboratory qualifications, and report format before production begins. International standards can help establish terminology and sampling concepts, but they do not automatically create acceptance criteria for your contract; align the chosen approach with the applicable market and product risk [1] [2].
Sampling, timing, and defect decisions
Sampling can control inspection effort, but it cannot eliminate uncertainty. A buyer should state the lot definition, sampling plan, inspection level, and acceptance and rejection numbers in advance. ANSI/ASQ Z1.4 is widely used as a reference for attribute sampling, while ISO 2859-1 provides an international framework for sampling procedures indexed by acceptance quality limit [1] [2]. Those frameworks require informed selection: an acceptance quality limit is not a promise that every shipment will contain only that defect rate. High-risk features may require one-hundred-percent checks or separate functional tests.
Schedule visits around production reality. A very early visit may reveal process problems but cannot verify finished output; a late visit may catch defects when there is no time to repair them. Tell the provider the planned quantity, completion percentage, packing status, and ship date, then require prompt notice if the factory changes the plan. If an inspection fails, freeze the decision path: record containment, request root-cause evidence, define rework boundaries, and authorize reinspection only after the agreed evidence is available. Never let a rushed vessel departure turn an unresolved finding into an assumed acceptance.
Verify the supplier and the inspection provider
Supplier verification should begin before the first purchase order. Match the legal entity on quotations, bank details, invoices, factory records, and contracts; confirm the actual production address; and ask who owns tooling, controls changes, and approves subcontracting. Review relevant process evidence, sample consistency, capacity assumptions, and references that can be independently checked. A factory may be an excellent fit for one product and unsuitable for another, so assess equipment and process capability against your own specification rather than relying on a broad product category or an online profile.
Evaluate the inspection company with the same discipline. Check its legal identity, geographic coverage, auditor experience, language capability, report controls, complaint route, and whether it can arrange competent laboratories without obscuring who performed the work. Ask how inspectors are trained, supervised, and assigned, and whether they can decline an assignment when impartiality is compromised. Where a management-system certification is presented, verify the certificate and scope through the relevant certification body or accreditation channel; a certificate alone does not prove that your product or shipment conforms [3].
Compliance, documentation, and corrective action
Compliance planning belongs in the specification, not as an afterthought after cartons are sealed. Identify the destination market, product classification, required labels, warnings, traceability marks, restricted substances, electrical or mechanical safety needs, and any importer records. Then distinguish documents that demonstrate a test, such as a laboratory report, from documents that demonstrate a supplier claim. Government agencies and recognized authorities publish product-specific obligations, and the responsible importer should confirm which rules apply to its exact goods and destination [3]. An inspection can observe labels and collect samples, but it cannot replace legal review or market authorization.
Require a corrective-action record for every significant nonconformity. It should name the defect, affected lot, suspected cause, immediate containment, proposed correction, responsible person, due date, supporting evidence, and verification method. Keep revision history for artwork, formulas, components, and packaging so an obsolete file cannot be used quietly. For recurring defects, trend the findings by supplier, line, product, and shift; then adjust training, tooling, incoming controls, or the purchase specification. Your quality file should preserve inspection reports, approvals, test records, correspondence, and final disposition for the retention period appropriate to the product and market.
Calculate the full cost and manage shipment risk
The inspection fee is only one part of the buying decision. Build a landed-cost view that includes product price, tooling, samples, laboratory testing, inspection or audit visits, rework, packaging changes, inland transport, export handling, freight, insurance, duties, brokerage, storage, destination delivery, payment charges, and a reasonable allowance for delays or rejected goods. Clarify the trade term and named place because responsibilities and included charges differ. Do not compare quotations using a factory price alone; compare the same specification, quantity, packaging, currency, delivery basis, and compliance scope.
Before release, reconcile the approved purchase order with the inspected lot and shipping paperwork. Confirm carton count, gross and net weights, dimensions, marks, pallet rules, container condition, and seal number where relevant. Establish who may authorize shipment, what happens if production is short, and how costs are allocated if rework or a second inspection is needed. A passing report should support a documented release decision, not create a delivery guarantee. Preserve a contingency plan for replacement production, partial shipment, or customer communication when evidence remains incomplete.
Buyer comparison of quality checkpoints
| Checkpoint | Best question answered | Buyer preparation |
|---|---|---|
| Supplier audit | Can this site and process plausibly support the order? | Legal identity, process map, capacity questions, and records |
| During-production inspection | Are materials and workmanship trending correctly before completion? | Risk list, work-in-progress timing, and defect examples |
| Pre-shipment inspection | Does a defined finished lot match the agreed specification? | Lot definition, sampling plan, acceptance limits, and approved sample |
| Laboratory testing | Does a sample meet the specified test method and limit? | Destination, method, sample custody, and qualified laboratory |
| Loading check | Are the correct goods packed, counted, marked, and secured? | Packing list, carton rules, container details, and release authority |
Buyer checklist
Use this before you request a quote
- Write a controlled specification with revision number, approved samples, measurable limits, packaging rules, and destination-market requirements.
- Verify the supplier’s legal identity, production address, subcontracting controls, capability evidence, and payment details before issuing the order.
- Select the inspection checkpoint, lot definition, sampling method, defect limits, test scope, report format, and escalation route in the purchase agreement.
- Confirm inspector competence, impartiality, instrument or laboratory controls, report traceability, and reinspection terms before the visit.
- Model landed cost and shipment contingencies, then release goods only after reconciling findings, corrective evidence, quantities, documents, and authorization.
References
- 1. [1] ASQ, ANSI/ASQ Z1.4 Sampling Procedures and Tables for Inspection by Attributes
- 2. [2] ISO, ISO 2859-1 Sampling procedures for inspection by attributes
- 3. [3] U.S. Consumer Product Safety Commission, Regulatory Robot and business compliance resources
This article provides general commercial information, not legal, tax, customs, product-safety, or regulatory advice. Confirm requirements for your product and destination before purchasing or importing.